Dextra Light
⚡ Featured UV Blacklight Series for New Amsterdam
Explore our top-tier commercial grade ultraviolet lighting solutions engineered for high durability, precision spectrum output, and robust operational stability.


📊 New Amsterdam Market Industrial & Commercial UV Landscape
An authoritative sector analysis detailing the integration of advanced UV blacklight applications within modern infrastructural, medical, and agricultural sectors.
🏙️ Strategic Industrial Integration in New Amsterdam
The evolving commercial landscape in New Amsterdam requires robust technological adaptations across multiple sectors. From advanced security verification systems in financial institutions and entertainment complexes to specialized agricultural curing and medical sterilization processes, the demand for precision UV blacklight lamps has expanded exponentially. Industrial operators require continuous operational uptime, stringent spectral compliance, and energy-efficient lighting frameworks that withstand local environmental variations.
Our manufacturing protocols align perfectly with these high standards, delivering stable UVA/UVC outputs and certified mercury-vapor containment or high-efficiency LED arrays. By bridging the gap between cutting-edge Chinese manufacturing capacities and New Amsterdam's industrial specifications, we ensure local enterprises gain unparalleled competitive edges through optimized lifecycle performance and minimal maintenance expenditures.
🌐 Macro Industry Solutions & Global Supply Chain Resilience
Global procurement managers demand absolute supply chain transparency, scalable manufacturing, and rigorous quality assurance. As an elite factory and direct supplier, we bypass traditional intermediaries to provide direct-to-market pricing and customized engineering. Whether it is large-scale municipal sanitation initiatives, commercial entertainment venue design, or precision non-destructive testing (NDT), our ultraviolet product ecosystem delivers reliable performance across more than 80 countries worldwide.
🏆 Why Choose Our UV Manufacturing Infrastructure
Demonstrating verifiable expertise, high production capability, and uncompromised quality assurance for international B2B buyers.
Advanced Production Capacity
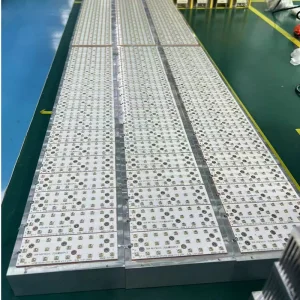
Four automated production lines and 36 high-speed placement machines support efficient, scalable, and high-precision manufacturing.
Quality Assurance
Every batch comes with a detailed inspection report, ensuring transparency and confidence for global buyers.
Global Sales Markets
Products are sold in over 80 countries across Europe, America, the Middle East, Africa, and Southeast Asia, backed by a complete sales network.
Customized Solutions
We analyze each client’s application scenario and business goal to design tailored solutions that deliver maximum value and efficiency.
🏢 Inside Zhongshan Dextra Lights Technology
Established in March 2012, our R&D team brings over 15 years of specialized experience in RGB display and UV industry engineering.
Enterprise Profile & Technical Backbone
Zhongshan Dextra Lights Technology is a private high-tech enterprise specializing in the production, sales, and R&D of multi-purpose LED display screens and excimer UV lamps. Backed by an initial capital investment of 10 million RMB, our facility covers approximately 9,000 square meters with over 120 skilled employees.
We maintain a fully equipped large-scale R&D center, a modern production hub, and perfect technical engineering test support driven by 10 professional domestic and international elites. Last year, total sales volume reached RMB 270 million, with UV products accounting for 37.8% and an annual sales growth rate exceeding 9.2%. Holding over 50 registered patents in China, innovation remains our core growth driver.
Comprehensive Application & Product Spectrum
Our core product portfolio includes indoor and outdoor LED displays, UV disinfection lamps, maternal and infant disinfection devices, pet sanitation and deodorization tools, UV semiconductors, UV air purification systems, and UV dust removal apparatus.
These advanced systems are extensively deployed in advertising media, stage performances, entertainment venues, celebrations, exhibitions, educational institutions, stadiums, public squares, shopping malls, transport hubs, airports, and marine ports worldwide.
🔬 Ultraviolet Purification & Engineering Mastery
Precision engineering designed to meet rigorous international sanitation and industrial irradiation standards.
Our engineering division applies strict thermal and electrical testing protocols to ensure every UV lamp tube operates within optimal peak wavelength tolerances (such as 365nm, 395nm, BLB fluorescent spectrum, and specialized UVC bands). This guarantees exceptional stability and prolonged operational lifespan for all commercial projects in New Amsterdam and beyond.
❓ Frequently Asked Questions (FAQ)
Expert answers regarding B2B procurement, technical specifications, and logistics for New Amsterdam clients.
💡 What wavelength is best for industrial inspection and curing?
Depending on your exact application, 365nm is ideal for precision inspection, forensic analysis, and adhesive curing, while 395nm and BLB (Blacklight Blue) are widely utilized for fluorescent effects, counterfeit detection, and pest control.
📦 Do you support OEM/ODM customization for New Amsterdam distributors?
Yes. We offer fully customizable branding, custom wattages, specialized lengths (such as T5, T8, T12 configurations), and tailored electrical ballasts matching regional voltage standards.
🚢 What are the typical lead times for international shipping?
With 4 automated production lines and 36 high-speed placement machines, standard production runs take between 15 to 25 days, backed by robust logistics partnerships serving over 80 countries.
🛡️ How do you ensure product quality before export?
Every single production batch undergoes rigorous spectral testing, electrical safety checks, and vibration stress analysis, and is shipped with an exhaustive factory inspection report.
📦 Complete UV Lamp & Blacklight Inventory
Browse our comprehensive selection of standard and high-power ultraviolet products engineered for global industrial and commercial deployment.